Alcohol 96% (Ethanol)
Introduction to Industrial Alcohol 96% (High-Purity Ethanol)
Alcohol 96%, universally known as rectified spirit or high-purity ethanol (C2H5OH), represents one of the most critical solvent and disinfectant bases used in modern production. It is an clear, colorless, and volatile liquid characterized by a distinct, pleasant odor and a sharp, burning taste. At a constant concentration of 96% volume, this chemical forms a natural azeotrope with water, making it the highest concentration of ethanol achievable through conventional, highly efficient fractional distillation.
When procuring this chemical on an international scale, quality definitions are critical. Iran Chemical Mine provides a premium, non-denatured agricultural and synthetic grade that adheres strictly to international pharmacopoeia and food safety benchmarks, ensuring trace impurities like methanol, aldehydes, and fusel oils remain far below toxicological thresholds.
Technical Characteristics and Grade Differences
Ethanol is generally categorized by its refined purity and intended end-use. For industrial buyers, understanding the contrast between medical/food-grade ethanol and standard denatured industrial variants determines chemical compatibility.
Food Grade and Medical Purity (Undenatured)
Food-grade Alcohol 96% is processed using agricultural raw materials like molasses, grains, or sugar beet. It must remain fully undenatured—meaning no toxic additives or bittering agents are introduced. It complies with FCC (Food Chemicals Codex) guidelines, making it completely safe for human consumption or skin contact applications.
Industrial Technical Grade (Denatured)
Technical-grade ethanol is regularly combined with small quantities of denaturants (such as isopropyl alcohol or MEK) to render it non-potable for tax or regulatory exemptions. This grade is primarily funneled into heavy paint solvent formulation, fuel mixtures, and screenwash production.
Comparative Purity Matrix
To assist procurement managers in evaluating raw materials, the table below highlights how Alcohol 96% compares to other common commercial alcohol grades:
| Parameter / Feature | Food & Medical Grade Alcohol 96% | Absolute Alcohol (99.9%) | Industrial Denatured Alcohol |
| Ethanol Content (v/v) | 95.6% – 96.5% | 99.5% – 99.9% | 90.0% – 95.0% |
| Water Content | ~4.0% | Less than 0.5% | 5.0% – 10.0% |
| Methanol Limits | Fewer than 10 ppm (Ultra Safe) | Less than 50 ppm | Elevated (Often added intentionally) |
| Denaturants Present | Absolutely None | Variable (Grade dependent) | Present (Pyridine, Wood Naphtha, etc.) |
| Primary Base Material | Agricultural / Sugar Fermentation | Synthetic / Dehydrated Ag | Petrochemical / Blended Run |
| Primary Industry | Food, Pharma, Cosmetics | Electronics, Fine Labs | Paints, Coatings, Fuel Brines |
Essential Industrial Applications of Alcohol 96%
Due to its high volatility, superb solvent capabilities, and non-toxic residual profile, Alcohol 96% serves as a foundation for multiple high-value industries.
1. Food and Beverage Processing
In the food industry, food-grade Ethanol 96% is indispensable. It acts as an extraction carrier for natural flavors, essential oils, and botanical colorings. Because it evaporates cleanly at low temperatures, it is used to fix aromatic essences and glaze confectionery items without altering the base taste. It also serves as a natural food preservative and surface sanitizer for commercial bakery packaging.
2. Pharmaceutical and Medical Sanitization
At a 96% baseline, this chemical is an elite sanitizer, heavily used to formulate hospital disinfectants, surgical scrubs, and high-efficiency hand rubs. Within pharmaceutical synthesis, it acts as a sterile solvent for precipitating proteins, extracting active pharmaceutical ingredients (APIs), and preserving liquid medications or tinctures.
3. Cosmetics and Personal Care Products
Premium perfumes, colognes, body mists, and hairsprays rely on high-purity undenatured alcohol as their primary delivery vehicle. It dissolves essential oils cleanly, ensures an immediate cooling effect upon skin application, and dries almost instantaneously without leaving sticky or unsightly chemical residues behind.
4. Chemical Syntheses and Laboratory Extraction
In specialized manufacturing, Alcohol 96% acts as a reaction medium for producing downstream chemical esters, plasticizers, and industrial adhesives. It is also utilized in extraction laboratories to separate organic compounds safely from botanical feedstocks.
Logistics, Fleet Safety, and specialized Transport
Because ethanol is highly flammable (Class 3 Hazardous Material), transport logistics demand exceptional equipment and rigorous regulatory oversight.
[Production / Refined Distillation]
                 │
                 ▼
[Dedicated Stainless Steel Tankers (SS316L)] ──► Prevent Corrosion & Maintain Food-Grade Purity
                 │
                 ▼
[Sealed Valves & Grounding Systems] ──────► Eliminate Ignition Risks & Volatile Evaporation
                 │
                 ▼
[Direct Cross-Border Custom Delivery] ───► High-Speed Supply Chain to Neighboring Markets
Stainless Steel Tanker Deliveries
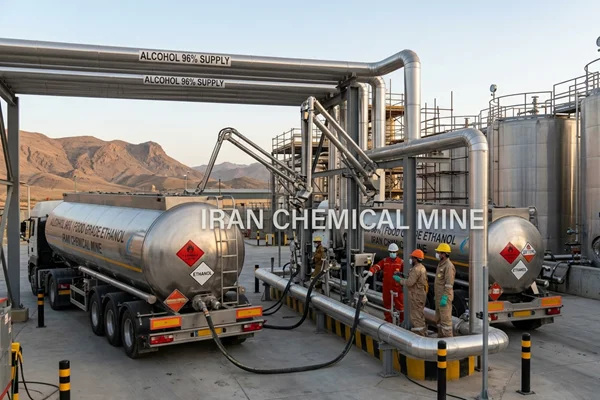
For high-volume neighboring markets, bulk shipping via dedicated Stainless Steel Tankers (SS316L) is mandatory. Standard steel or plastic-lined tanks run a high risk of leaching iron ions or chemical plasticizers into the product, destroying the food-grade status.
Iran Chemical Mine utilizes a proprietary fleet of pristine, chemically isolated stainless steel road tankers. These tankers are structurally engineered to prevent chemical cross-contamination, safeguard proof levels from ambient moisture intake, and resist temperature fluctuations.
Safe Handling Protocols
Every single bulk delivery vessel is armed with vapor-recovery systems, emergency pressure valves, and robust copper static-grounding lines to neutralize friction-induced sparks during high-speed loading and offloading cycles.
Strategic Export Destinations
Leveraging our geographic proximity and streamlined customs clearance pathways, Iran Chemical Mine coordinates high-speed distribution channels across several prominent economic corridors:
-
CIS and Central Asia: Turkmenistan, Uzbekistan, Tajikistan, Kazakhstan, and Armenia (supporting booming pharmaceutical and manufacturing sectors).
-
Middle East & Neighboring Countries: Iraq, Turkey, Pakistan, Afghanistan, and the UAE (supplying bulk sanitizer formulation plants and food processing hubs).
-
East Africa & Caucasus: Azerbaijan, Georgia, and Oman (servicing cosmetic manufacturing and industrial solvent blenders).
Why Buy Alcohol 96% from Iran Chemical Mine?
Selecting a chemical partner requires verifying batch uniformity, logistical safety, and absolute supply consistency. Iran Chemical Mine stands as an elite, authorized supplier specializing in bulk ethanol delivery.
Unyielding Quality Controls
Every batch of Alcohol 96% distributed by Iran Chemical Mine is backed by an independent gas chromatography mass spectrometry (GC-MS) analysis report. We strictly control volatile organic impurities, ensuring absolute adherence to European Pharmacopoeia (EP) and United States Pharmacopeia (USP) requirements.
Seamless Supply Chain Continuity
With our specialized bulk handling facilities and dedicated cross-border road tanker networks, we eliminate transit delays and intermediate handling risks. Whether your production lines demand immediate food-grade compliance certification or a reliable high-volume industrial solvent stream, Iran Chemical Mine delivers unmatched technical accuracy, competitive pricing, and secure, door-to-door bulk shipping.
